
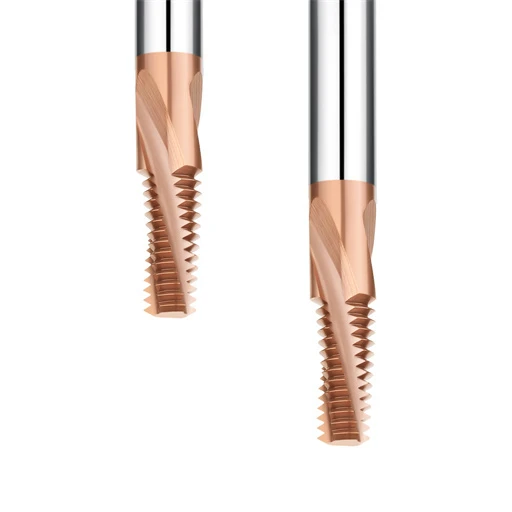
HRC65 Thread Mill Geometry: How to Choose the Right Geometry for Hardened Steel
Recently, a Detroit stamping die customer contacted our engineering team with an urgent production bottleneck. They were milling M6×1.0 blind threads into D2 tool steel hardened to 63–65 HRC using high-rigidity 5-axis vertical machining centers and shrink-fit tool holders. Standard tooling chipped within the first pass, and when a tool finally finished a hole, the
HRC65 Thread Mill Geometry: How to Choose the Right Geometry for Hardened Steel Read More »