
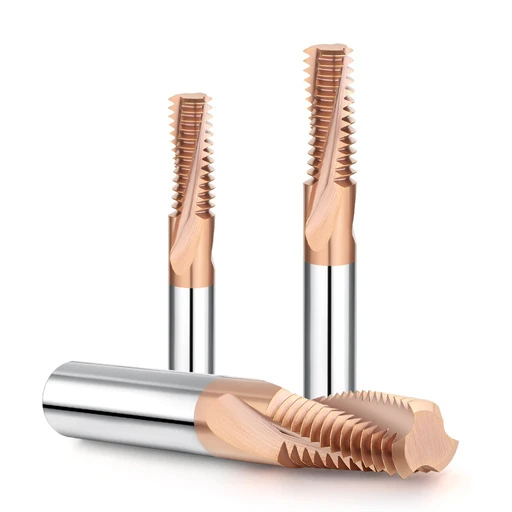
Thread Mill Flute Geometry for Hardened Steel: Flute Design for HRC60–65 Thread Milling
Three months ago, a German client making stamping dies reached out with an urgent bottleneck. They were milling M6×1.0 blind-hole threads into CPM 10V inserts hardened to HRC 62–64 using a commercial carbide tool. Every tool chipped at the tooth tip by the third hole. Macro-fracture inspection showed no standard flank wear or torque breakage.
Thread Mill Flute Geometry for Hardened Steel: Flute Design for HRC60–65 Thread Milling Read More »