SAMHO

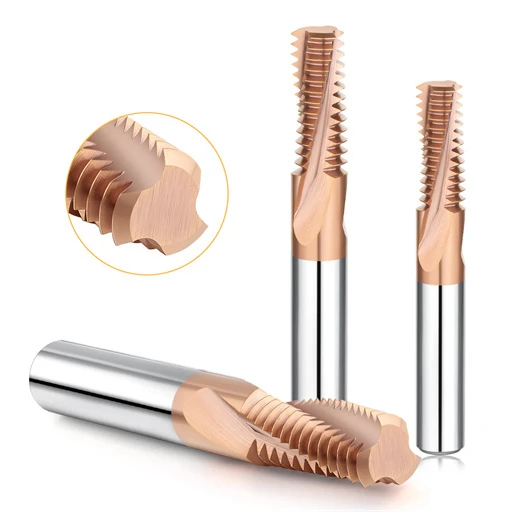
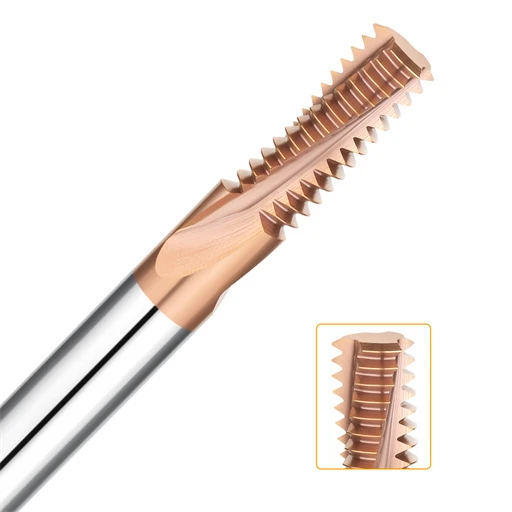
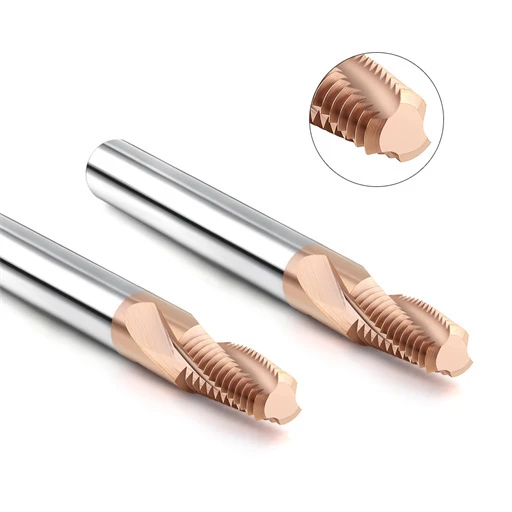
HRC65 full tooth thread cutter

How to Reduce HRC65 Thread Mill Tool Wear in Hardened Steel

This scenario unfolded on our shop floor during a technical call with a German mold manufacturer. The job ran an SKD11 slide insert heat-treated to a measured HRC65 with M6×1.0 blind holes. The operator tore through three brand-new carbide thread mills in a row; none made it past hole eight. Under our 200x bench microscope,

How to Reduce HRC65 Thread Mill Tool Wear in Hardened Steel Read More »
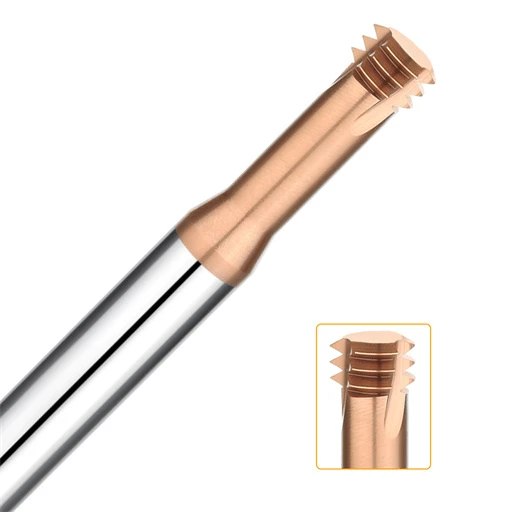
thread cutting end mill​

How to Troubleshoot Thread Mill Vibration in Hardened Steel

A precision injection mold shop in Ohio called us with an urgent problem: machining M6×1.0 threads into AISI H13 inserts hardened to HRC 58–60. Mid-cycle, the spindle began emitting a piercing screech. When the operators stopped the machine, they found wavy micro-spalling across the thread flanks. Worse, the No-Go gauge slipped right in, and tool

How to Troubleshoot Thread Mill Vibration in Hardened Steel Read More »

HRC65 full tooth thread cutter

7 Common Causes of Thread Mill Breakage in HRC65 Steel

While machining double-cryogenically tempered SKD11 stamping die inserts, a long-time client called us with a critical issue. They were milling M4×0.7 blind-hole threads in stable HRC65 steel. Their solid carbide tool suffered a brittle fracture near the shank root before completing even two full revolutions. The snapped tool jammed deep inside the cavity, putting an

7 Common Causes of Thread Mill Breakage in HRC65 Steel Read More »

thread end mill

Micro Thread Milling Strategy for HRC65 Hardened Steel

Last month, we helped a German contract manufacturer troubleshoot a high-stakes job. The workpiece was Böhler M390 powder-metallurgy steel, heat-treated to an actual hardness of HRC 64–65. They needed to cut 48 blind-hole M1.6×0.35 threads at a challenging 2.8D depth-to-diameter ratio. Their process engineer broke four consecutive cutters at the neck transition and the first

Micro Thread Milling Strategy for HRC65 Hardened Steel Read More »

thread mills

Deep Hole Thread Milling in HRC65 Steel: Tool Selection, Cutting Strategy, and Accuracy Control

Last month, a long-standing partner—a precision injection mold shop in Stuttgart, Germany—sent us a video from their shop floor. A 5-axis machining center had triggered an emergency stop with a broken tool fragment wedged at the bottom of a hole. The workpiece was a D2 tool steel mold insert valued at tens of thousands of

Deep Hole Thread Milling in HRC65 Steel: Tool Selection, Cutting Strategy, and Accuracy Control Read More »

thread mills

External Thread Milling in Hardened Steel: Toolpath Strategies and Cutting Tips

Last month, a mold shop in Stuttgart sent a scrapped ejector guide pin to our lab. The part was vacuum-hardened AISI D2 tool steel (1.2379) at 62 HRC with an M16×1.5 external thread. The shop tried single-point threading on a lathe. They shattered three coated inserts in a row. After 14 hours of upstream machining,

External Thread Milling in Hardened Steel: Toolpath Strategies and Cutting Tips Read More »

thread mills

HRC65 Internal Thread Milling: Tool Selection and Machining Strategies

Last winter, a long-standing client in Stuttgart reached out with an urgent problem. They needed to add four M6 internal threaded holes to a D2 stamping die insert. The block was already vacuum-hardened to HRC64–65. The operator tried to tap the holes with a standard carbide tap, but it snapped after engaging just two threads.

HRC65 Internal Thread Milling: Tool Selection and Machining Strategies Read More »

thread mills

HRC65 Thread Milling Strategy for Precision Mold and Die Machining

Late last year, we were called to troubleshoot a tooling crisis at a German precision mold shop. The team was threading a powder-metallurgy steel insert hardened to HRC 64–65.5. The part had already undergone dozens of hours of EDM, finish milling, and vacuum heat treatment. A shop floor technician attempted to tap an 18 mm

HRC65 Thread Milling Strategy for Precision Mold and Die Machining Read More »

thread mills

How to Calculate Thread Milling Parameters for HRC65 Steel

Last month, a German mold-making client emailed us photos of two broken solid carbide thread mills snapped inside blind holes, along with a scrapped powder-metallurgy die insert. The workpiece was vacuum heat-treated cold-work steel hardened to a punishing HRC65. The shop ran standard catalog speeds and feeds. The tool micro-chipped on pass one and sheared

How to Calculate Thread Milling Parameters for HRC65 Steel Read More »

thread mills

CNC Thread Milling Circular Interpolation Parameters for Hardened Steel

Last month, we assisted an automotive stamping die manufacturer in Stuttgart, Germany, with a critical failure on their shop floor. A set of SKD11 progressive die inserts—valued at over €40,000—failed during the finish-milling of M10×1.5 threads after heat treatment to HRC 60. Less than three seconds after the operator started the cycle on a five-axis

CNC Thread Milling Circular Interpolation Parameters for Hardened Steel Read More »