SAMHO

graphite end mill

Why 4 Flute Graphite End Mills Are Preferred for High Precision Graphite Machining

In precision mold manufacturing and EDM electrode production, achieving tight tolerances on brittle materials requires optimized tooling. Standard 2-flute cutters often cause problems during graphite finishing operations. As cutting depths increase, machinists frequently observe poor surface finishes, rapid tool wear, and severe graphite edge chipping. A high-density graphite electrode project recently highlighted this challenge during

Why 4 Flute Graphite End Mills Are Preferred for High Precision Graphite Machining Read More »
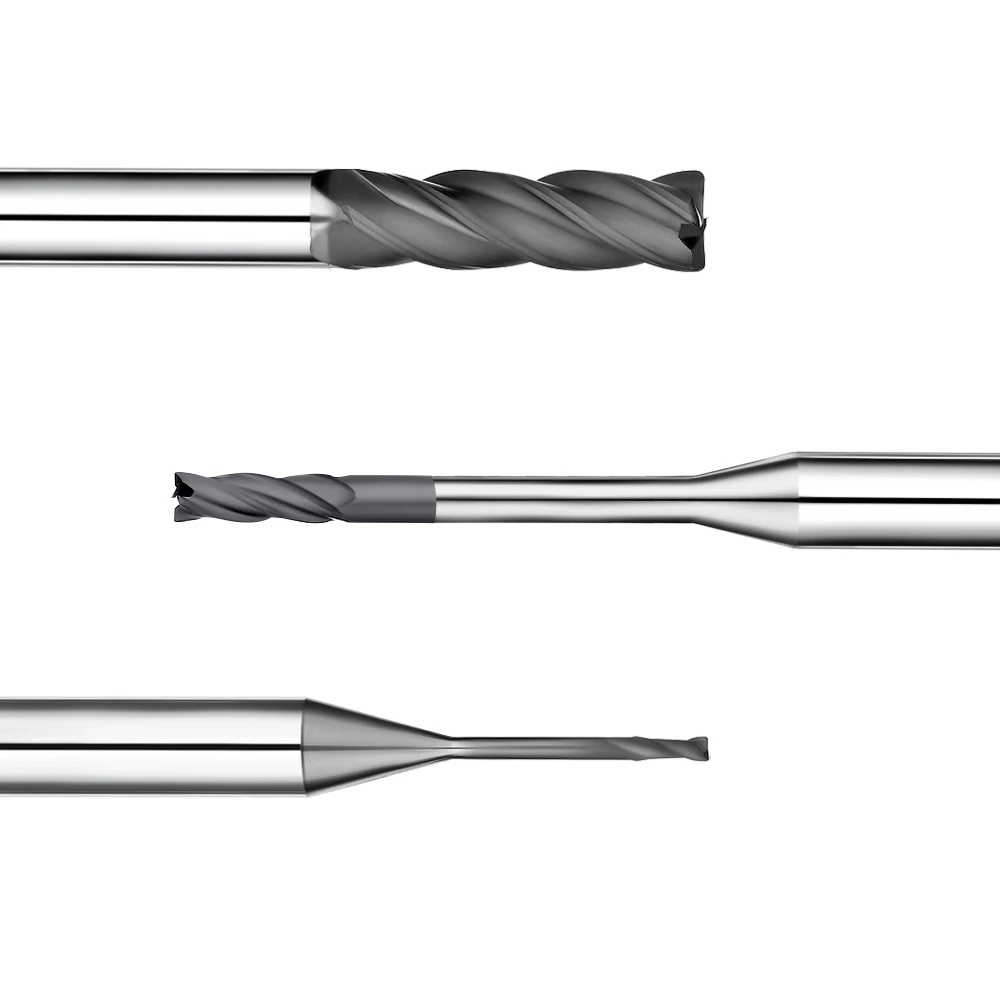
graphite end mill

1 Flute vs 2 Flute vs 4 Flute Graphite End Mill: How to Choose the Right Flute Number for Graphite Machining

During a recent graphite electrode machining project, our field team ran into a classic problem. A client ran various graphite grades on the same high-speed CNC center, yet saw massive variations in tool wear, surface finish, and cycle times. Our on-site analysis proved the issue was not just feeds and speeds—it came down to an

1 Flute vs 2 Flute vs 4 Flute Graphite End Mill: How to Choose the Right Flute Number for Graphite Machining Read More »

diamond coated end mills for graphite

How to Extend Graphite End Mill Tool Life in CNC Graphite Machining

In practical EDM graphite electrode machining, engineers often face a frustrating challenge: two shops running the exact same grade of graphite, CNC equipment, and tooling can see drastically different results. While one achieves stable, extended runs, the other deals with rapid edge wear, chipping, and lost electrode tolerances within hours. We saw this firsthand with

How to Extend Graphite End Mill Tool Life in CNC Graphite Machining Read More »

graphite end mill

What Causes Rapid Tool Wear in Graphite Machining? How to Extend Graphite End Mill Tool Life

A client recently reached out regarding a graphite electrode machining project where standard carbide tools were failing prematurely. While initial parts passed inspection, the cutting edges dulled rapidly during continuous runs. Dust generation surged, tool change frequency spiked, and profile accuracy degraded. The customer assumed the graphite grade was defective, but our on-site analysis revealed

What Causes Rapid Tool Wear in Graphite Machining? How to Extend Graphite End Mill Tool Life Read More »

graphite milling tools

Why Do Graphite End Mills Wear Quickly? Understanding Tool Life and Improving Machining Performance

In precision graphite machining, a familiar pattern often frustrates machinists. A brand-new graphite end mill performs smoothly at first. Then, after several hours—or just dozens of cycles—the surface finish deteriorates, dimensions begin to drift, and micro-chipping appears on the cutting edge. Strangely, different machine shops running the same grade of graphite with identical cutting tools

Why Do Graphite End Mills Wear Quickly? Understanding Tool Life and Improving Machining Performance Read More »

diamond end mill cutting tools

Why 4 Flute Graphite End Mills Work Better for CNC Graphite Machining?

In practical project optimization, we often see a recurring issue: shops run into varying results when swapping tools, even while keeping the same cutting parameters. We once consulted for a mold manufacturer producing high-density graphite EDM electrodes. During initial trials, they used 2-flute graphite end mills for cavity roughing and semi-finishing. While these tools completed

Why 4 Flute Graphite End Mills Work Better for CNC Graphite Machining? Read More »

6-flutes-end-mills

The Role of Flute Count in End Mills for Metal: 2, 4, or 6 Flutes?

A few months ago, we helped a long-established German machine shop resolve a classic machining disaster. They were using 4-flute carbide square end mills to clear slots in 7075 aluminum alloy on a newly installed high-speed machining center. Within less than half an hour, chips jammed the slots, snapping the tool and triggering an emergency

The Role of Flute Count in End Mills for Metal: 2, 4, or 6 Flutes? Read More »

diamond end mill cutting tools

1 Flute vs 2 Flute End Mill for Graphite Machining: A Complete Tool Selection Guide

While engineering a graphite electrode machining solution for a European mold-making client, we encountered a classic shop floor dilemma. The client relied on high-speed machining centers to produce complex EDM graphite electrodes. However, their engineering team struggled to decide whether a 1-flute or 2-flute graphite end mill was the optimal choice for their operation. Initially,

1 Flute vs 2 Flute End Mill for Graphite Machining: A Complete Tool Selection Guide Read More »

diamond coated end mills for graphite

Dry vs Wet Graphite Machining: How to Choose the Right Machining Strategy for Graphite CNC Applications

While optimizing a graphite electrode setup for a European mold manufacturer, we faced a classic challenge. The client was using wet machining to lower temperatures, but suffered from inconsistent surface finishes. Even worse, graphite dust mixed with coolant formed a sticky sludge inside the machine, severely reducing the service life of their graphite milling cutters.

Dry vs Wet Graphite Machining: How to Choose the Right Machining Strategy for Graphite CNC Applications Read More »

diamond coated end mills for graphite

How to Choose the Right Depth of Cut for Graphite End Mills During CNC Graphite Machining

While optimizing a graphite electrode process for a European mold maker, we encountered a common pitfall: using a single graphite end mill at a fixed depth of cut across varying cavity depths. Initial cuts were smooth, but deeper passes caused subtle edge chipping. This micro-chipping degraded the surface finish, making the finished electrodes fail strict

How to Choose the Right Depth of Cut for Graphite End Mills During CNC Graphite Machining Read More »